
- SPC Cpk = 1.851 (one characteristic on one part, not a blanket capability claim) on a representative length characteristic (76.1–76.5 mm), against an initial-study target of Ppk ≥ 1.67.
- In-house metrology: Hexagon CMMs, vision machines, XRF, hardness, salt spray, and tensile testers.
- Full APQP/PPAP: process flow, control plan, SPC, and PFMEA produced in-house.
- Material checked at the door: XRF against the mill certificate on every incoming lot.
What process capability does this shop actually hold?
"We hold tight tolerances" is cheap; a Cpk number is not. On a representative length characteristic — 76.1–76.5 mm, measured across 25 subgroups of 4 samples — the SPC record shows Cpk = 1.851 (one characteristic on one part, not a blanket capability claim), judged OK against an initial-study target of Ppk ≥ 1.67. General characteristics target Cpk ≥ 1.33.
Read the number correctly: Ppk ≥ 1.67 initial means the process spread fits comfortably inside the tolerance band with margin to spare — the difference between "we measured a good part once" and "the process stays in control across a run."
The Cpk number is also how two shops that both print "±0.003 mm (milling) / ±0.002 mm (turning)" get separated. One shows you the chart behind the claim; the other repeats the claim. The chart is the difference between a process you can audit and a sentence you have to trust, and it is the first thing to request when the tolerance matters.
How are critical dimensions measured?
On equipment a buyer would use to audit the shop, not on a pair of calipers. The in-house bench includes two Hexagon CMMs (up to 900 × 1500 × 800 mm), vision measuring machines, a gear measuring center, and surface roughness and profile instruments. A dimension is either proven on these or it is not guaranteed.
The class of equipment matters because it sets the ceiling on what can be verified. A shop that measures with calipers can promise any tolerance it likes and never be caught; a shop that measures on a CMM has to be right, because the instrument records the number whether it passes or fails.
Measurement is also a question of where it happens. A dimension checked on the shop's own CMM, a few meters from the machine that cut it, can be re-checked in minutes and corrected the same day. A dimension checked off-site waits for a courier before the correction starts. In-house metrology is not a convenience; it is the speed of the quality loop.
How is incoming material verified?
Quality starts before any metal is cut. Every incoming lot is checked by XRF spectrometer against its mill certificate, so a substituted or mislabeled alloy is caught at the door rather than shipped inside your parts. This is the same discipline IATF 16949 audits look for, and it runs on every job, not just automotive ones.
The XRF check is fast enough to run on every lot precisely because it is handheld and non-destructive. That is what makes it a real control instead of a spot check: it does not sample a few bars, it reads every incoming lot against its certificate, and it catches the wrong alloy while it is still sitting on the dock.
What is the full inspection equipment list?
The 20+ instrument bench covers dimensional, material, surface, and mechanical verification:
| Category | Equipment |
|---|---|
| Dimensional | Hexagon GLOBAL S CMMs (2), CMM-686, CNC-322, Hexagon OPTIV & VIEWMAX vision machines, ZD20 gear measuring center |
| Surface | KEYENCE VK-X3000 laser microscope, SURFCOM 1800D, Mitutoyo roughness tester, ACCRETECH profile |
| Material | iCHEQ handheld XRF/PMI spectrometer |
| Mechanical | HVS-1000A micro-Vickers hardness, Fischer coating thickness, salt-spray chamber, tensile tester |
The list is long because no single instrument covers everything. A CMM proves dimensions, a vision machine proves small features and edges, the XRF proves chemistry, and the hardness and tensile gear prove mechanical properties. Together the bench covers the four things you can be lied to about: size, shape, material, and strength.
Does the factory produce APQP and PPAP documentation?
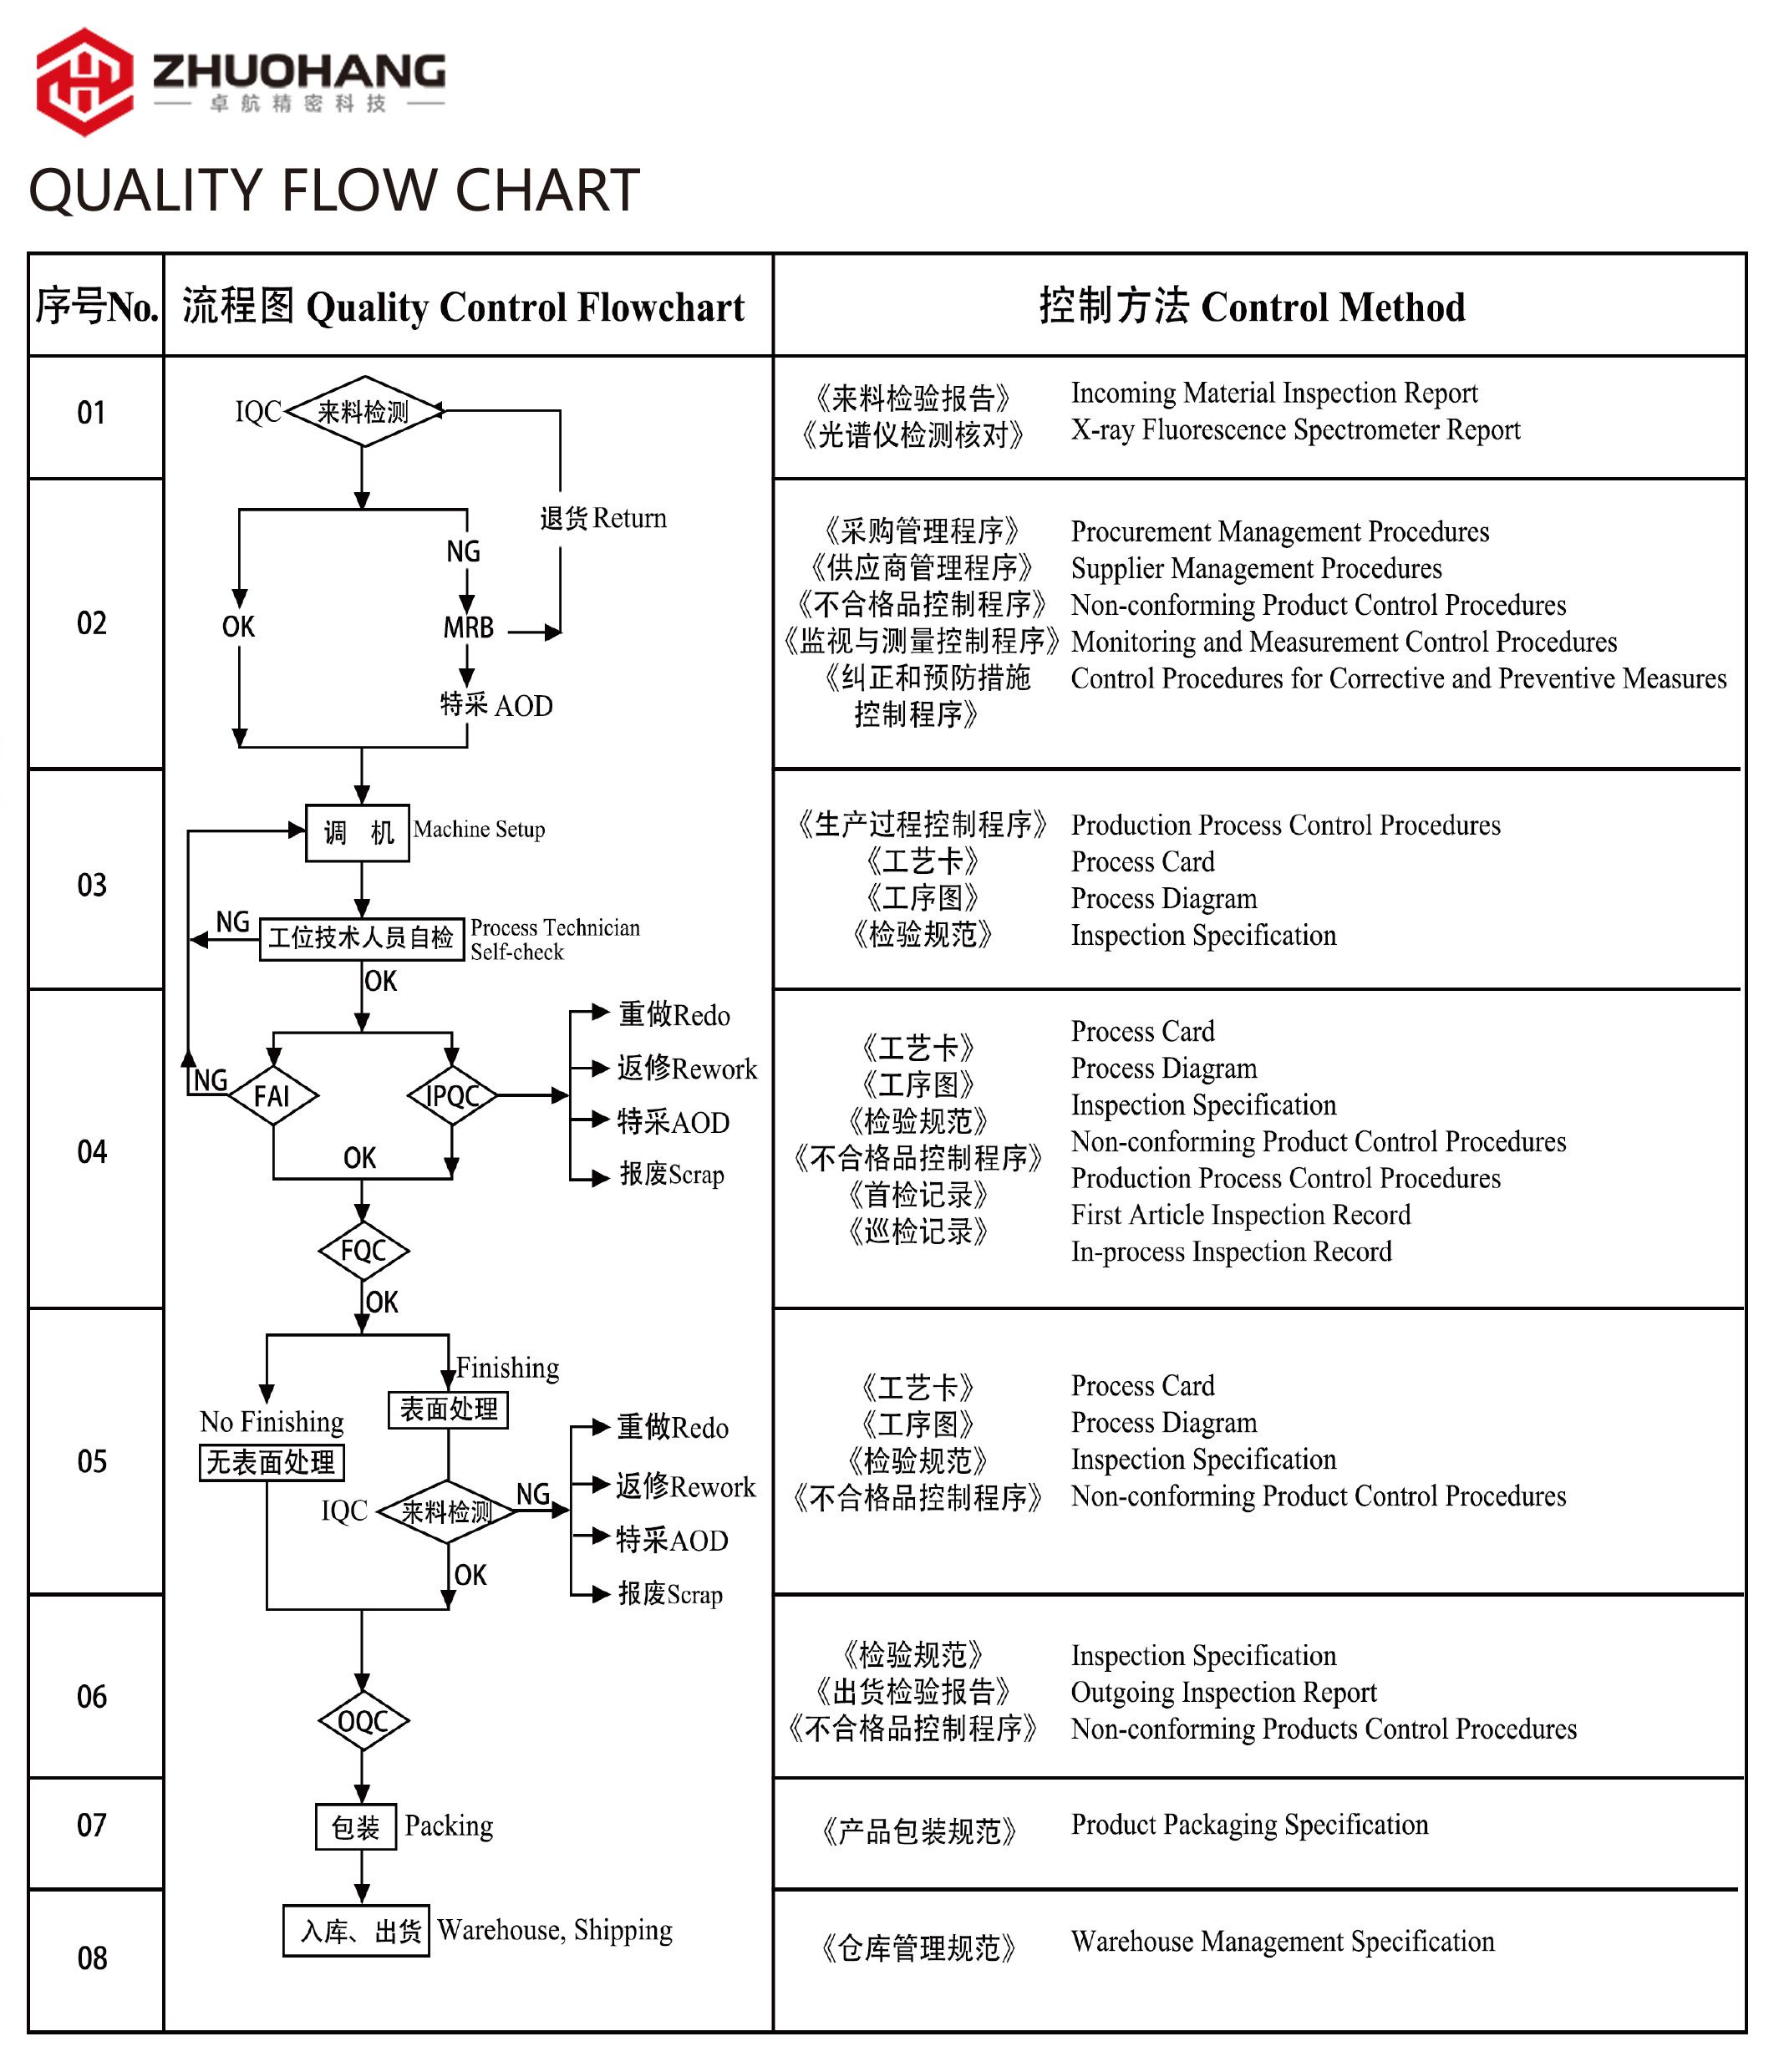
Yes, and this is where the IATF 16949 certificate shows up in practice. For automotive programs the factory produces the full quality package — process flow chart, control plan, SPC control charts, and PFMEA — in-house, rather than asking the buyer to assemble the documentation from a pile of vendor promises. A representative customer program delivered all four, plus noise/waste-water/air pollution control procedures.
The package is produced in-house rather than assembled from vendor promises, which matters when a customer or an auditor asks for it. A control plan written by the shop that runs the process is a real document; a control plan pasted together from templates is a form. Ask to see a real one from a past program and read the details — they will tell you which kind you are holding.
How does traceability run through a batch?
The MES/ERP system records the full chain on every lot: raw material source and usage, process parameters, machine data, production batch, machining time, operator, and inspection results. If a non-conformance surfaces, the factory can isolate which lot, which machine, and which operator produced it — instead of quarantining an entire shipment on a guess.
Traceability also protects you in the normal case, not just the failure case. When the records travel with the lot, you can verify after delivery that the material, the machine, and the operator were what the shop said they were. The record is the shop's memory, and a shop that keeps good records is a shop that can be held to them.
What should you ask for as evidence of quality?


Whether you buy here or elsewhere, the evidence a serious shop can produce on request is specific:
- An SPC chart from a real job, not a capability statement. Ask for the Cpk, the subgroup structure, and the date.
- A CMM report against your drawing. A dimensional report you can read is the whole point of inspection.
- A material certificate plus the XRF check. Two independent confirmations beat one.
- The APQP/PPAP package for automotive work. If the shop cannot produce a control plan, it is not running IATF-level process control.
This facility will produce all of them in writing, before you commit.
Why is Cpk a better claim than a tolerance?
A tolerance says where the part must land; Cpk says how reliably it lands there. A shop can hit ±0.003 mm (milling) / ±0.002 mm (turning) once and drift on the next ten parts. Cpk measures the spread of a whole run against the tolerance band, so it answers the question the tolerance alone cannot: will the next part be good, or was the last one lucky?
That is why capability is the claim a serious buyer asks for. It turns a one-part anecdote into a process-level fact, and it is the number an auditor can check against the actual control charts. A tolerance is a target; Cpk is whether the process is aimed at it.
What does Ppk ≥ 1.67 initial versus Cpk ≥ 1.33 mean for your part?
The two thresholds exist because not every dimension is equally critical. A general feature can tolerate a process that fits the band with a slimmer margin, so Cpk ≥ 1.33 is enough. A critical feature — a bearing bore, a seal face — needs the wider margin of Ppk ≥ 1.67 initial, because a drift there is a functional failure, not a cosmetic one.
| Characteristic class | Target | What it means |
|---|---|---|
| Key characteristics | Ppk ≥ 1.67 initial | Critical features get a wide safety margin |
| General characteristics | Cpk ≥ 1.33 | Non-critical features get a standard margin |
The split is why you mark critical dimensions on the drawing. It tells the shop where to concentrate its SPC effort, and it tells you where to look first when you audit the charts.
How does a CMM report prove a dimension, and what should it contain?
A CMM report is a dimension's birth certificate. It should name the drawing revision, list each measured feature against its tolerance, show the measured value and the deviation, and state whether it passed. A report that omits the drawing revision, or lists only some features, is evidence of something — just not of your part.
The report matters because it is the point where the tolerance claim meets the physical part. When the prototype arrives with a CMM report against your drawing, you are not trusting a promise; you are reading a measurement. Ask for the report to ship with the parts, and check the revision against what you approved.
What goes into an APQP/PPAP package, and why does it matter?
APQP is the planning method; PPAP is the evidence package it produces. Together they answer, before production, the questions a failure would force you to ask afterward: what is the process, what can go wrong, how is it controlled, and how is it measured. For automotive work, the factory produces the full package in-house — process flow chart, control plan, SPC charts, and PFMEA.
- Process flow chart — the sequence of every operation on the part.
- PFMEA — what can fail at each step and how it is prevented.
- Control plan, which dimensions are checked, how, and how often.
- SPC charts — the process staying in control, in data form.
The package matters because it is the difference between managing quality and hoping for it. A shop that can produce all four is running IATF-level process control; a shop that cannot is assembling parts and calling it production.
How does SPC catch drift before it ships a bad part?
SPC watches the process, not the parts. It plots measurements over time and flags a trend before the process walks out of tolerance — a tool wearing, a fixture loosening, a temperature shift. The chart catches the drift early, when the part is still good, instead of waiting until a bad part is already measured and rejected.
That is the difference between inspection and control. Inspection finds the bad part after it is made; SPC stops the process before it makes one. When you see a control chart on a critical dimension, you are seeing the shop catch its own drift, which is exactly what you want it to do when you are not watching.
How do you distinguish a real SPC chart from a marketing one?
A real control chart has a structure you can verify: the characteristic it tracks, the tolerance limits, the control limits, the subgroup size, and the dates. A marketing chart is a smooth line with no axis labels and no way to check it. The difference is visible in seconds.
Here the representative chart is specific: a length characteristic of 76.1–76.5 mm, measured across 25 subgroups of 4 samples, showing Cpk = 1.851 (one characteristic on one part, not a blanket capability claim), judged OK against a Ppk ≥ 1.67 initial-study target. When a shop gives you a chart, ask for that same level of detail — the subgroup structure, the date, and the characteristic. A chart that cannot name its own parts is not evidence.
How do the equipment list and the tolerance claims line up?
Every tolerance claim should map to an instrument that can check it. ±0.003 mm (milling) / ±0.002 mm (turning) and ±0.002 mm are not numbers a caliper can prove; they need CMMs, vision machines, and profile instruments. When you read the equipment list, read it as the proof behind the tolerance: the CMMs prove the dimensions, the XRF proves the material, the hardness and tensile gear prove the mechanical properties.
| Claim | Instrument that proves it |
|---|---|
| ±0.003 mm (milling) / ±0.002 mm (turning) / ±0.002 mm | Hexagon CMMs, vision machines, profile instruments |
| Material grade | iCHEQ XRF/PMI spectrometer |
| Hardness and mechanical properties | Micro-Vickers and Rockwell testers, tensile tester |
| Surface and corrosion | Roughness testers, salt-spray chamber, coating gauge |
A shop that lists the instruments behind each claim is a shop that expects to be audited. A shop that lists tolerances without instruments is asking you to take the number on faith.
How does quality evidence change what you can commit to?
Evidence is what turns a supplier into a decision. With the Cpk chart, the CMM report, and the material certificate in hand, you are not betting on a promise — you are committing to a documented process. Without them, every production order is a leap of faith, and a leap of faith is not a procurement strategy.
The whole quality page exists to make that commitment cheap. The evidence is produced on every job, not just the automotive ones, and it ships with the parts when you ask. That is the difference between a supplier you audit and a supplier you trust, and it is the difference this page is about.
A compact version of the evidence request, for any supplier:
- The Cpk chart for the critical dimension, with subgroup structure and date.
- A CMM report against your drawing revision.
- The material certificate and the matching XRF reading.
- The control plan and PFMEA if the part is automotive.
Request all four and read what comes back. A shop that sends real charts and reports is showing you its process; a shop that sends paragraphs is showing you its brochure.
Why does the evidence run on every job, not just automotive ones?
The discipline of SPC, CMM inspection, and XRF material checks does not switch on when an automotive buyer calls and off when a prototype buyer does. It runs on every job because the equipment and the procedures are the same regardless of the part number. A shop that only tightens up for automotive is telling you it can relax the rest of the time, and relaxed is not what you want on your parts.
The benefit flows to every buyer. A prototype machined under the same SPC and CMM discipline as a production automotive part carries the same evidence trail, whether or not your industry demands it. You get the rigor without paying a premium for the label.
How do you put the evidence to work in your own decision?
The evidence is only useful if you use it. When the quote comes back, ask for the Cpk chart, the sample CMM report, and the material certificate as part of the same conversation. A supplier that sends them without hesitation is a supplier you can move forward with; a supplier that stalls has told you what its "quality" is made of.
The verification does not end at the order, either. When the parts arrive, match the reports to the drawing revision and the heat number, and file them. That file is your traceability on the buyer side — the evidence that turns a good supplier into a documented one, and the difference between buying a part and buying a guarantee.
What this shop actually runs
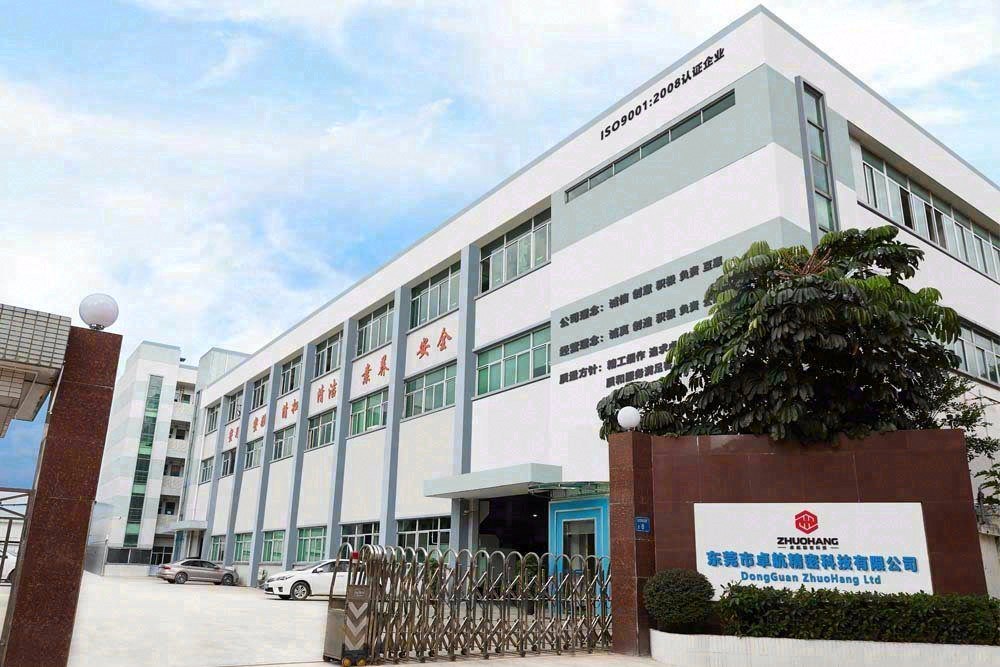
Ask for capability evidence and the answer should be specific. The facility behind this guide runs 100+ CNC machines on a 6,800 m2 floor in Dongguan, China, with 100+ staff. The machine list, by category:
- 5-axis machining centres (10+) - Mazak VARIAXIS I-600 (510/910/510 mm travel, 12,000 rpm, 22 kW, 71.6 N·m, 30-tool BT40) and Mazak INTEGREX I-250H S (B-axis 0.0001°, 24 kW, 124 N·m, 38-tool HSK-A63). Meant for compound-angle parts, single-setup multi-face prismatic work, and aerospace fittings where datum transfer loss is unacceptable.
- 3-axis / 4-axis machining centres (50+) - Brother SPEEDIO S500Z2N / S700Z2N (10,000 rpm, 14/21-tool ATC, 0.7 s tool-to-tool, Z-axis 2.2 G) and Mazak VCE-430A L / VCE-570C L (10,000 rpm, 118 N·m, 24-tool ATC). Meant for prismatic parts, plates, brackets, housings.
- Swiss-type turning centres (10+) - Citizen Cincom A20-3F7 (Φ20 mm, 10,000 rpm), TSUGAMI B0206-III / B0205-III (Φ20 mm, 0.1 µm), STAR SR-32JII / SR-32J Type N (Φ32 mm, 8,000 rpm). Meant for long, slender rotational parts at ±0.002 mm.
- CNC turning centres (20+) - HEADMAN T70M/1250 (720 mm swing, 117 mm bore, 3,000 rpm, BMT75 12-station turret). Meant for shafts, bushings, flanges up to ±0.002 mm.
- Wire EDM (5+) - Sodick AQ535L (550/350/300 mm travel, ±20° taper, 800 kg workpiece). Meant for hardened tool steel, internal splines, sharp internal corners that milling cannot reach.
- Inspection: Hexagon CMM + 20+ gauges - Hexagon CMM for coordinate measurement, plus vision system, profilometer, hardness tester, coating thickness gauge, XRF for material verification. The 10:1 rule (gauge 10x more accurate than the band) is applied to every feature.
- Machine highlights - VARIAXIS I-600: one-setup multi-face 5-axis + MAZA-CHECK auto-calibration; INTEGREX I-250H S: DONE-IN-ONE mill-turn, B-axis 0.0001° + Ai thermal shield; SPEEDIO S500Z2N / S700Z2N: Z-axis 2.2 G + 0.7 s ATC; Swiss-type: guide-bush switchable + 0.1 µm resolution.
Tolerances held: milling ±0.003 mm, turning ±0.002 mm, grinding and wire EDM ±0.002 mm. Capability: Ppk >= 1.67 initial and Cpk >= 1.33 in production on key characteristics.
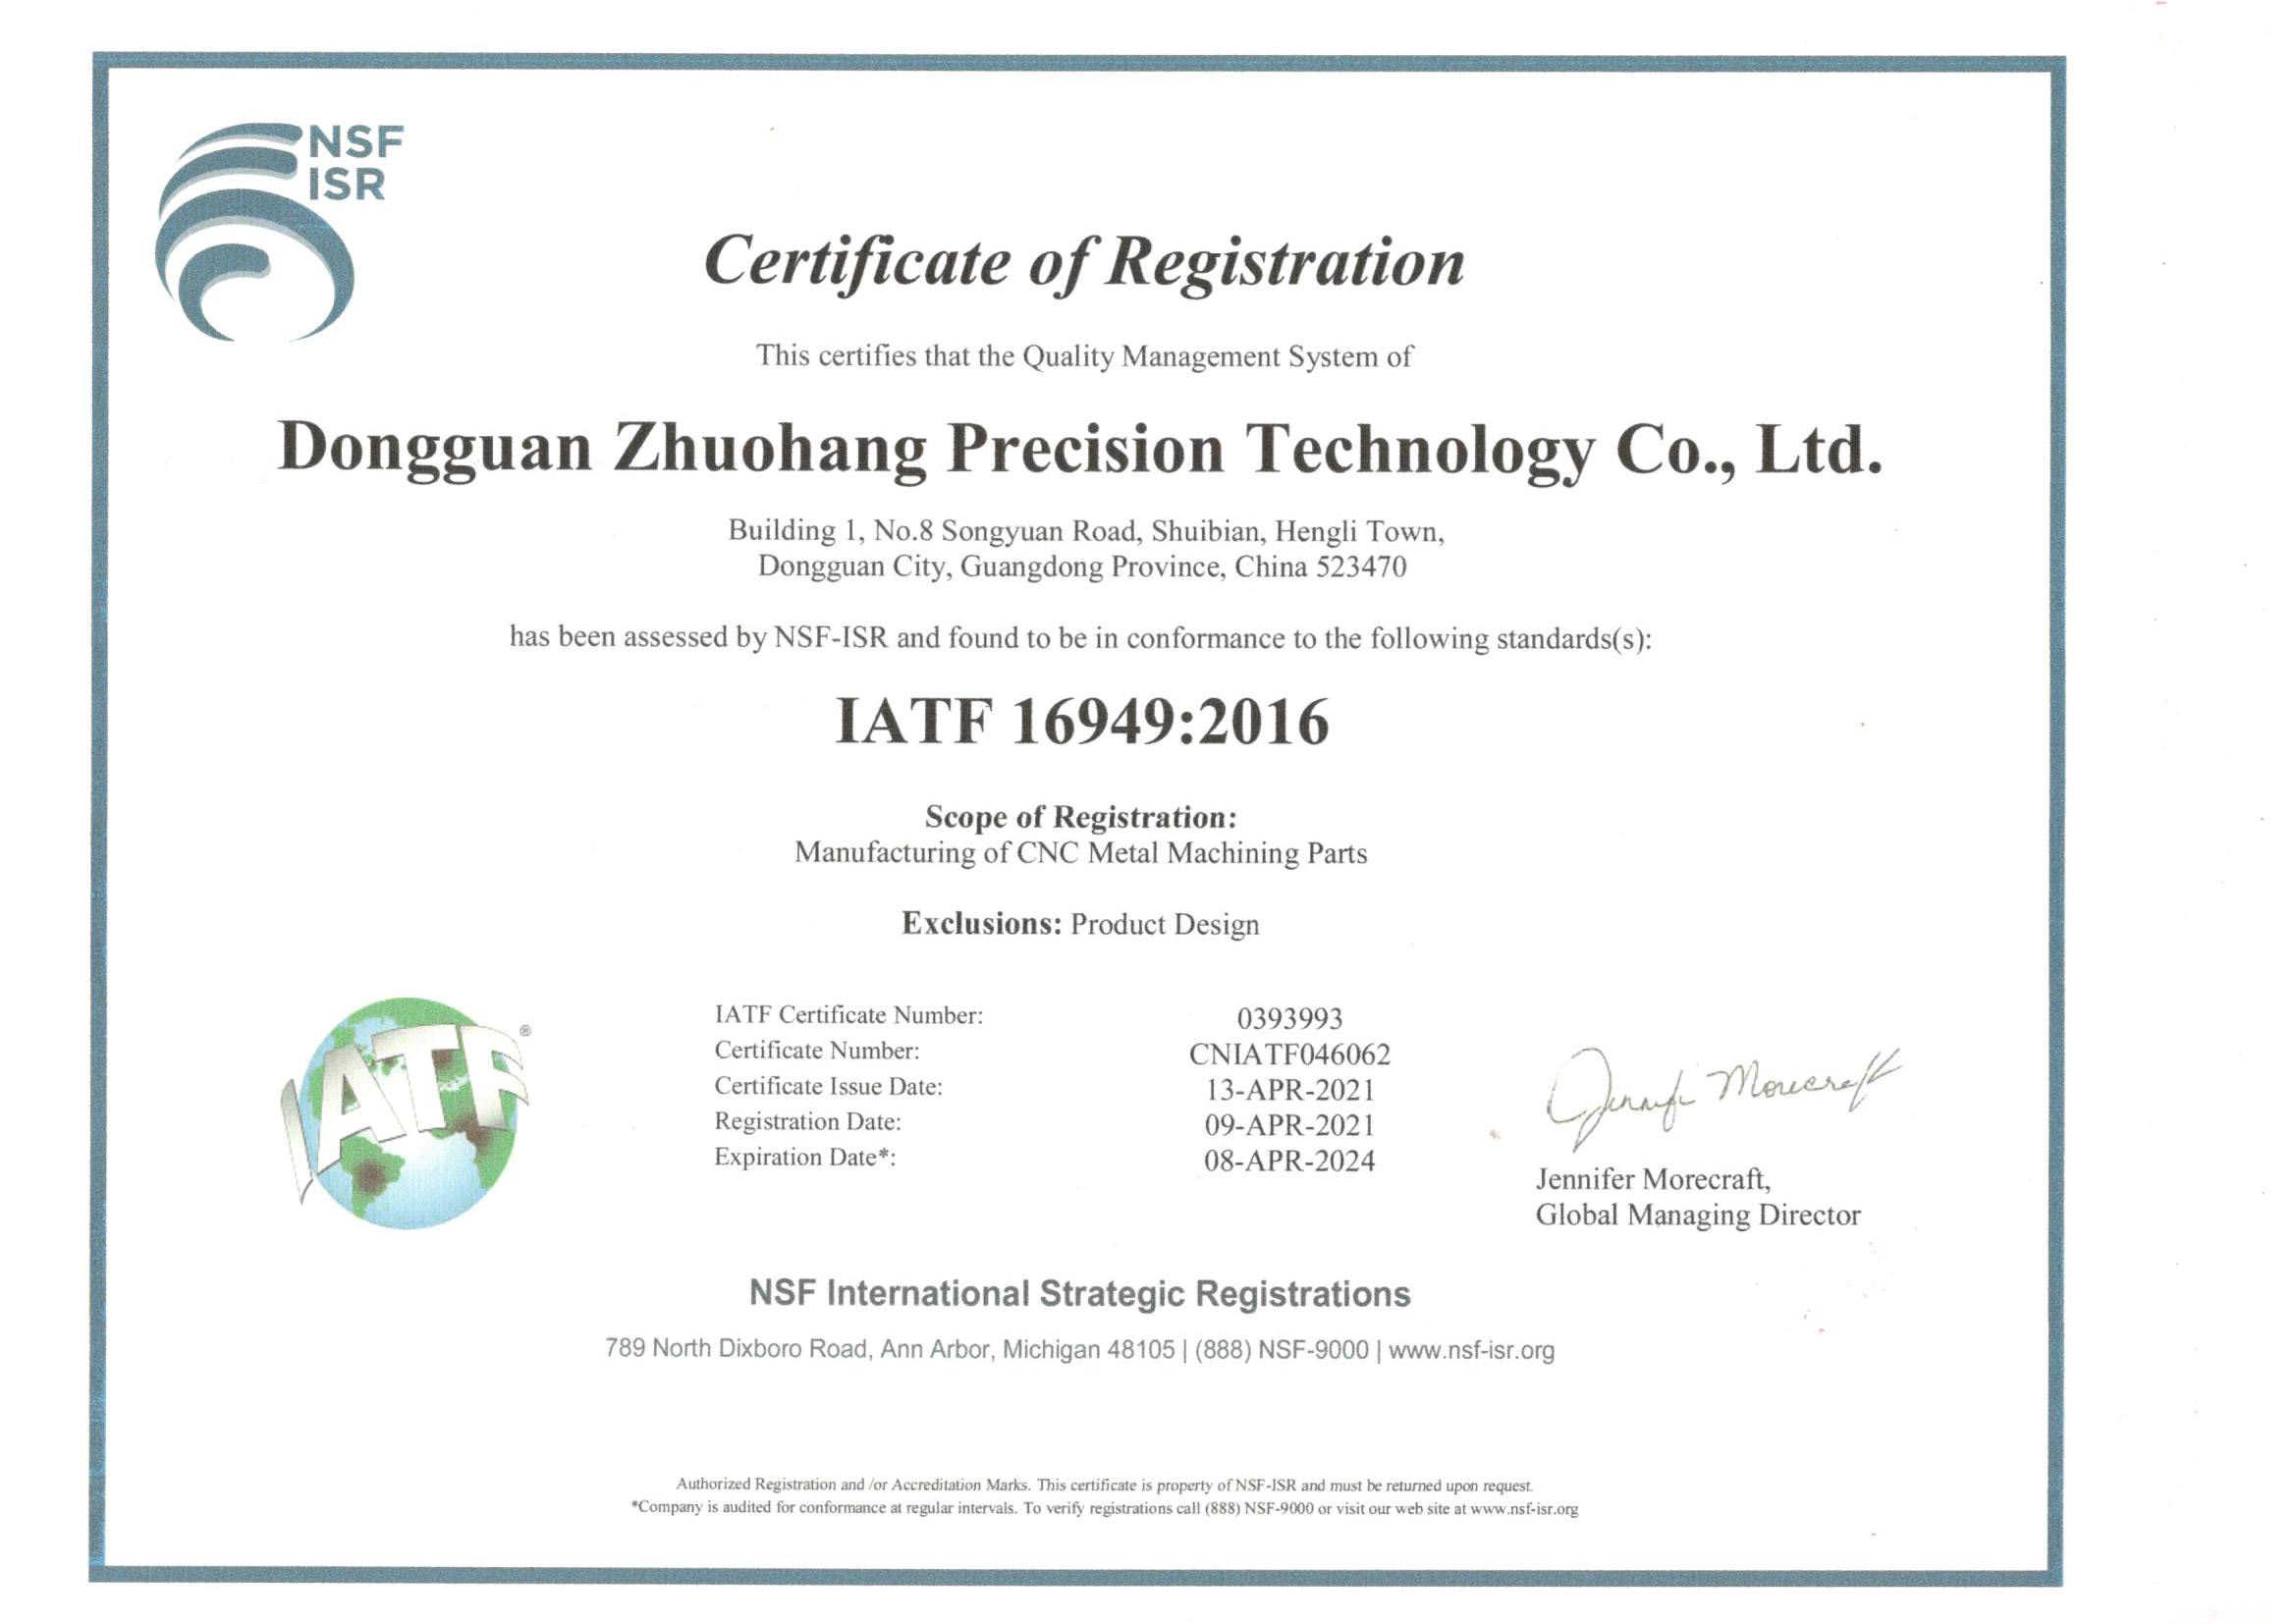
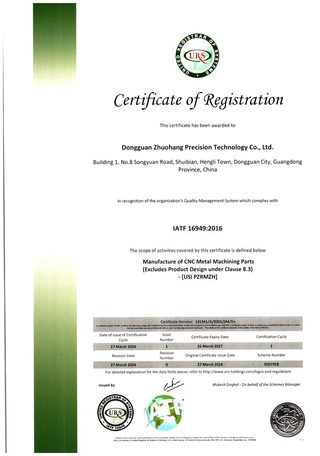
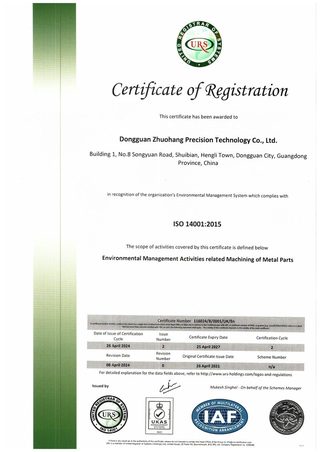
Certifications: ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En, clause 8.3 design excluded, disclosed openly) and ISO 14001:2015 (116024/B/0001/UK/En), issued to Dongguan Zhuohang Ltd, USCC 91441900MA4UWT6X39, established 2005.
Service area: Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa — built in China, shipped worldwide.
Contact: Felipe Iglesias, [email protected], +86 13126536955.
Want the quality evidence before you order?
Ask for the SPC chart and a sample CMM report — send your drawing to [email protected] or call +86 13126536955.
Frequently Asked Questions
What process capability do you hold on key characteristics?
In short, Key characteristics target Ppk ≥ 1.67 initial and general characteristics Cpk ≥ 1.33. A representative length characteristic (76.1–76.5 mm) shows Cpk = 1.851 (one characteristic on one part, not a blanket capability claim) across 25 subgroups of 4 samples, judged OK.
How are critical dimensions measured?
On Hexagon CMMs, vision measuring machines, and a gear measuring center, backed by surface roughness and profile instruments. The inspection bench is the same class of equipment a buyer would use to audit the factory.
How is incoming material verified?
Every incoming lot is checked by XRF spectrometer against its mill certificate before machining, so mixed or mislabeled stock is caught at the door rather than shipped in your parts.
Do you provide APQP and PPAP documentation?
Yes. For automotive work the factory produces the full package — process flow chart, control plan, SPC charts, and PFMEA — rather than asking you to assemble the quality documentation yourself.
What inspection equipment do you run in-house?
Hexagon CMMs, vision measuring machines, an XRF spectrometer, micro-Vickers and Rockwell hardness testers, a coating thickness gauge, a salt-spray chamber, and a tensile tester — 20+ instruments in total.
Do inspection reports ship with the parts?
Yes. CMM inspection reports, SPC charts, and material certificates ship with the parts on request, so you receive documented evidence of what was measured and what it was made from.
Which certifications back the quality system?
In short, ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En), and ISO 14001:2015 (116024/B/0001/UK/En), all issued against Dongguan Zhuohang Ltd and verifiable with the registrar, with each scope stated honestly in the certificate itself.
China CNC Prototype Quality — Related Pages
Continue reading: China CNC Prototype Factory · China CNC Prototype Services · China CNC Prototype Parts Manufacturer
Standards referenced on this page
- IATF 16949:2016 — Automotive quality management system standard
- ASTM A582/A582M-12 — Standard Specification for Free-Machining Stainless Steel Bars
- ASTM E8/E8M-21 — Standard Test Methods for Tension Testing of Metallic Materials